Plant28718 OK-112, Poteau, OK 74953

ScheduleRunning 24/7

Call(918) 649-0065 Emailcontact@polydynellc.com

Presses · Resins · Secondary work

Our Capabilities

Between our line-up of injection molding machines, and the array of materials we process, we are able to complete a wide variety of projects with ease.

From tooling validation through 24/7 production runs, insert molding, decoration, and secondary assembly, we take technical resins to a finished, packed part.

Presses on the floor
11
Clamp force range
30–600 t
Shot size range
1.76–143 oz
Resin families processed
6

Equipment fleet

Injection molding machines

The press list, as it stands on the floor. It accommodates micro parts through large multi-pound components without sending work outside.

Polydyne LLC injection molding press fleet, by clamp tonnage, machine make, and shot size.
Clamp force Machine make Shot size
30 ton Cincinnati 1.76 oz.
50 ton Demag (2) 4.5 oz.
120 ton VanDorn 8 oz.
135 ton Haitian 8.7 oz.
165 ton Intellect 8.7 oz.
170 ton VanDorn 8 oz.
170 ton Demag 14.7 oz.
300 ton Demag 40.3 oz.
400 ton VanDorn 48 oz.
500 ton VanDorn 60 oz.
600 ton Haitian 143 oz.
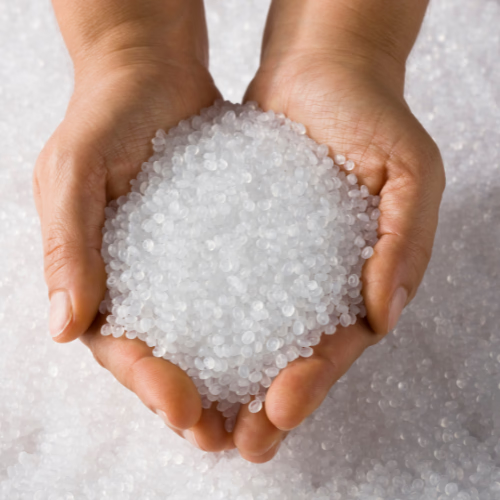
A handful of virgin thermoplastic resin pellets before drying and molding
Resin, as received Every job starts here. Incoming resin is checked and dried before it reaches a barrel.

Process control

The machine settings are evidence, not guesswork

Our presses carry computerised closed-loop monitoring that records melt temperature, injection pressure, hold time, and cooling on every cycle. When a part drifts, the record shows where.

Combined with robotic part drop and temperature-controlled molds, that keeps geometry inside print across millions of cycles rather than across the first thousand.

Specialties

Core molding and assembly services

Four processes, all under one roof in Poteau. A part can be moulded, fitted with inserts, decorated, assembled, and packed without leaving the building.

Primary process

01

Custom Plastic Injection Molding

A versatile fleet of presses under closed-loop process control. Part weights run from fractional grams to multi-pound components.

  • Multi-cavity production tooling
  • Micro-tolerance repeatability
  • Robotic part extraction
  • 24/7 continuous running

Integration

02

Insert & Encapsulation Molding

Metal inserts, brass threaded bushings, electrical contacts, and structural fasteners encapsulated inside the moulded geometry.

  • Brass and steel insert loading
  • Electrical pin encapsulation
  • High pull-out retention
  • Automated insert placement

Finishing

03

Part Decoration & Hot Stamping

Decorative finishing in house: high-temperature foil hot stamping, pad printing, colour matching, and multi-colour logo work.

  • Foil hot stamping
  • Precision pad printing
  • Textured and gloss finishes
  • Wear-resistant inks

Secondary work

04

Ultrasonic Welding & Sub-Assembly

Ultrasonic welding, heat staking, snap-fit integration, and unit testing so parts leave the plant assembled and checked.

  • Ultrasonic plastic welding
  • Heat staking and thermal insertion
  • Sub-component testing and kitting
  • Custom protective packaging

Materials processed

Engineering thermoplastics we run

We mold engineering-grade technical resins and commodity polymers. If your print calls for a grade that is not listed, ask; the list is what we run, not what we can run.

  • ABS & Polycarbonate

    Impact resistance, dimensional stability, optical clarity, housing enclosures.

  • Nylon (PA6 / PA66)

    High thermal resistance, wear resistance, glass-filled structural grades.

  • Delrin / Acetal (POM)

    Low friction coefficient, high stiffness, precision gears and bushings.

  • Polypropylene & Polyethylene

    Chemical resistance, living hinges, food-grade containers, flexible caps.

  • TPE / TPU Elastomers

    Overmoulded soft grips, flexible seals, vibration dampening components.

  • PBT & Engineered Blends

    High dielectric strength, flame-retardant electrical housings.

First article inspection record for a moulded housing A sectioned housing drawing carrying overall length 96.40 millimetres plus or minus 0.08, height 58.20 millimetres plus or minus 0.05, two 8.00 millimetre reamed bosses, and a 2.5 millimetre corner radius, recorded against print revision C. 96.40 ± 0.08 58.20 ± 0.05 2 × Ø 8.00 H7 R 2.5 Record First article Part Housing, stepped Print revision C Result Pass
Inspection record Every run opens with a measured part and closes with an audit. The print decides, not the press.

Quality and metrology

Measured before it ships, not after it fails

Quality sits in the process, not at the end of it. Incoming resin is checked, the first article is measured against the print, and statistical checks continue through the run.

Optical comparators, precision calipers, moisture analysers, and custom check fixtures decide whether a box leaves the building.

Request a capability assessment

Send the print. We will tell you which press it runs on.